跳至主要内容

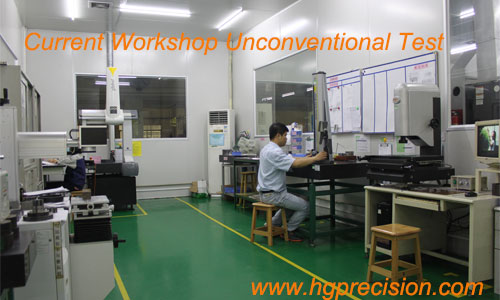
Current Workshop Unconventional Test

 As we know,every CNC Machinery Parts products need to test and check before selling out.And they would be tested repeatly.Now we will say about the Current Workshop Unconventional Test for the CNC machining parts.

1: Detection of inner diameter
When the workpiece can not be directly measured with the inside micrometer, the following methods can be referred to for inspection.
  • For the workpiece with wall thickness less than 30, first measure the outer circle size of the workpiece, and then measure the wall thickness size with a sharp divider, that is, the inner hole size = the outer circle size -2* the wall thickness size. This method can be controlled within 0.005.,
  • Measure the size of the hole by means of the table. First measure the size of the workpiece's outer circle. Then measure the size of the outer circle and the wall thickness with the table.This method can also be controlled within 0.005.
  • Check the hole size with the plug gauge of corresponding size.
  • THE CNC lathe can first finish the inner hole, see the light of the outer circle, send the product for three times of inspection, and change the way of filling the knife.
2. Measurement of short interval difference outer circle:
  • Numerical control equipment can be measured by means of calibration table, while non-numerical control equipment can be measured by means of pad gauge directly using micrometer card.That is, the outer circle size of the segment difference = the size of the pad gauge - the size of the block gauge.
  • First, measure the size of the outer circle. The size of the marking section difference is equal to the size of the outer circle -2* the marking section difference.
  • The CNC lathe can first finish the inner hole, the outer circle to see the light, and the product to be inspected for three times
Current Workshop Unconventional Test - HG

After measurement, rewrite the way of knife filling.

Visual quality requirements
  • The appearance of the parts should not rust. Solution: oil the parts in time to prevent rust after processing.
  • There should be no scratches on the appearance of the parts. Solutions: the bottom surface of the workpiece can be filled with paper in the clamping process, and the workpiece can be placed with plastic box in the handling process. The workpiece should not be superimposed as far as possible.
  • The sharp corners, adjacent edges and planes of the workpiece should not be damaged. Solution: pay attention to the handling and handling of the workpiece. The sharp corners parts should be wrapped with white tape.

评论

此博客中的热门博文

What is Guide Pin ?

  1.Definition of guide pin The  guide pin  is a guide element used in the mold in combination with the components to ensure that the mold moves and guides the mold stroke with precise positioning. They are generally cylindrical with shoulders and usually have oil grooves. 2.The material of the guide pin The material of the  guide pin  is generally selected from bearing steel, hot work die steel, easy car iron, etc., and the use of bearing steel SUJ2 is larger, which greatly enhances the durability and interchangeability of the guide post in terms of guiding performance. The guide post and components constitute the outer guide post component and the inner guide post component, which have a beautiful metallic luster. Heat treatment of guide post: HRC58-62; surface roughness of guide post: Ra0.8, Ra1.6. 3.Center hole of guide pin The roundness of the  guide pin  is very demanding. The central hole is mainly used to grind the outer diameter with a cylindr...

What's the properties of POM?

  Polyformaldehyde (POM) thermoplastic crystalline polymer. Known as "Super Steel" or "Sai Steel", The English abbreviation is POM. Generally, polymers obtained by formaldehyde polymerization have a low degree of polymerization and are easily thermally depolymerized. It can be used as a raw material for organic chemicals and synthetic resins, and as a fumigant for drugs. 1.General property POM  is a hard, dense material with a smooth surface and gloss, light yellow or white, thin-walled partly translucent. Combustion characteristics are easy to burn, and continue to burn after leaving the ignition source. The flame is yellow at the upper end and blue at the lower end. Melting dripping occurs and has a strong pungent formaldehyde smell and fishy smell. POM is white powder, usually opaque, good coloring, specific gravity 1.41-1.43 g/cm3, molding shrinkage 1.2-3.0%, molding temperature 170-200℃, drying conditions 80-90℃ for 2 hours. POM's long-term heat resistance ...

Precision CNC Milling Service: What Factors Affect CNC Machining Cost?

  How to save CNC milling costs? Why some custom  CNC milling services  are expensive? Firstly, we may need to know the cost factors for CNC milling services. 1)Stock Material As with any type of manufacturing, Stock material is the most basic cost. Some materials are more difficult to process than others, and some materials are more expensive as raw materials. The processing speed of some materials is much slower than others, even with the advancement of modern tools and mechanical technology. Some materials can wear out the expensive consumable cutting tools used more quickly, and can vary from one tool that makes hundreds or even thousands of parts to one part consuming multiple tools.Therefore, the material selection of your components can be a huge cost factor. 2)The Specification of  CNC Machining Parts The size and overall geometry of the parts are of course important factors in the quotation of machining operations. Obviously, the larger the physical part, th...